
ASTM A53 pipe-aSTM A53 grade b,a specification steel pipe
Pandapipe offers ASTM A53 Grade A and B pipe piles, as well as SMLS and ERW steel pipes. Make sure you get high quality, high performance steel pipe.

ASTM A53
- Name: ASTM A53 carbon steel pipe
- Manufacturing: ERW, seamless
- DN: 6 to 650
- NPS: 1/8 to 26 inches
- Outer DIA.: 10.3 to 660.4 mm
- Steel Grade: Grade A, Grade B
- Wall Thickness: 1.65 to 25.4 mm (SCH 5S to SCH XXS)
- Scope: fluid transportation, structural applications, high-temperature services, pressure systems, etc.
- ASTM A53 PDF Download
ASTM A53 is a standard specification published by the American Society for Testing and Materials (ASTM) for seamless and welded black pipe as well as hot-dipped galvanised steel pipe. He includes three pipe types Type F (furnace welded pipe), Type E (resistance welded pipe) and Type S (seamless pipe), with two grades, Grade A (lower strength) and Grade B (higher strength). The standard is primarily used for mechanical and pressure applications, but is also suitable for general use in steam, water, gas and air pipework.
ASTM A53 Pipe Processes
Production process
Seamless pipe and welded pipe with steel production process is very strict, the main use of flat furnace, electric furnace or alkaline oxygen method of these three processes, each process has its advantages and characteristics, in the production process may use one or more processes to ensure that the chemical properties of the steel pipe, mechanical properties, etc. to meet the production standards.
hot treatment
For welds in Class B E or F pipe, to ensure that no untempered martensite remains in the weld area, heat treat or other process after welding to a temperature of at least 1,000°F (540°C), and then continue the heat after reaching a certain temperature, to ensure that the temperature is uniformly distributed and that the material is fully transformed.
Cold Expansion Process
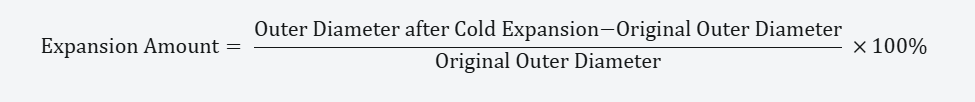
In order to achieve a close fit when connecting or repairing pipes, we often use the cold expansion process in (expansion refers to the amount of change in the diameter of the pipe in the process of cold expansion), but in order to ensure the performance of the material, the integrity of the structure, etc., the expansion amount shall not exceed 1% of the original outside diameter of the pipe.
Calculation of the amount of expansion shall be based on the outer diameter (OD) of the pipe using the following formula:
ASTM A53 Pipe Specification Sizes Chart
ASTM A53 carbon steel tubes to meet the specific needs of your different projects. We offer you pipes for ERW and seamless manufacturing processes. We manufacture pipes in strict accordance with ASTM A53 standards, and strictly control the quality of materials, dimensions, wall thickness, chemical composition and mechanical properties.
| Steel Pipe Dimensions Chart ANSI B36. 10 & 36.19 | ||||||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Nominal Pipe Size | Outside Diameter (mm) | Nominal Wall Thickness Schedule | ||||||||||||||
| NPS | DN | OD | SCH 5 | SCH 10 | SCH 20 | SCH 30 | SCH Sth | SCH 40 | SCH 60 | SCH XS | SCH 80 | SCH 100 | SCH 120 | SCH 140 | SCH 160 | SCH XXS |
| 1/8 | 6 | 10.3 | 1.24 | 1.45 | 1.73 | 1.73 | 2.41 | 2.41 | ||||||||
| 1/4 | 8 | 13.7 | 1.65 | 1.85 | 2.24 | 2.24 | 3.02 | 3.02 | ||||||||
| 3/8 | 10 | 17.1 | 1.65 | 1.85 | 2.31 | 2.31 | 3.20 | 3.20 | ||||||||
| 1/2 | 15 | 21.3 | 1.65 | 2.11 | 2.41 | 2.77 | 2.77 | 3.73 | 3.73 | 4.78 | 7.47 | |||||
| 3/4 | 20 | 26.7 | 1.65 | 2.11 | 2.41 | 2.87 | 2.87 | 3.91 | 3.91 | 5.56 | 7.82 | |||||
| 1 | 25 | 33.4 | 1.65 | 2.77 | 2.9 | 3.38 | 3.38 | 4.55 | 4.55 | 6.35 | 9.09 | |||||
| 1 1/4 | 32 | 42.2 | 1.65 | 2.77 | 2.97 | 3.56 | 3.56 | 4.85 | 4.85 | 6.35 | 9.70 | |||||
| 1 1/2 | 40 | 48.3 | 1.65 | 2.77 | 3.18 | 3.68 | 3.68 | 5.08 | 5.08 | 7.14 | 10.15 | |||||
| 2 | 50 | 60.3 | 1.65 | 2.77 | 3.18 | 3.91 | 3.91 | 5.54 | 5.54 | 8.74 | 11.07 | |||||
| 2 1/2 | 65 | 73 | 2.11 | 3.05 | 4.78 | 5.16 | 5.16 | 7.01 | 7.01 | 9.53 | 14.02 | |||||
| 3 | 80 | 88.9 | 2.11 | 3.05 | 4.78 | 5.49 | 5.49 | 7.62 | 7.62 | 11.13 | 15.24 | |||||
| 3 1/2 | 90 | 101.6 | 2.11 | 3.05 | 4.78 | 5.74 | 5.74 | 8.08 | 8.08 | |||||||
| 4 | 100 | 114.3 | 2.11 | 3.05 | 4.78 | 6.02 | 6.02 | 8.56 | 8.56 | 11.13 | 13.49 | 17.12 | ||||
| 5 | 125 | 141.3 | 2.77 | 3.40 | 6.55 | 6.55 | 9.53 | 9.53 | 12.70 | 15.88 | 19.05 | |||||
| 6 | 150 | 168.3 | 2.77 | 3.40 | 7.11 | 7.11 | 10.97 | 10.97 | 14.27 | 18.26 | 21.95 | |||||
| 8 | 200 | 219.1 | 2.77 | 3.76 | 6.35 | 7.04 | 8.18 | 8.18 | 10.31 | 12.70 | 12.70 | 15.09 | 18.26 | 20.62 | 23.01 | 22.23 |
| 10 | 250 | 273.0 | 3.40 | 4.19 | 6.35 | 7.80 | 9.27 | 9.27 | 12.70 | 12.70 | 15.09 | 18.26 | 21.44 | 25.40 | 28.58 | 25.40 |
| 12 | 300 | 323.8 | 3.96 | 4.57 | 6.35 | 8.38 | 9.53 | 10.31 | 14.27 | 12.70 | 17.48 | 21.44 | 25.40 | 28.58 | 33.32 | 25.40 |
| 14 | 350 | 355.6 | 3.96 | 6.35 | 7.92 | 9.53 | 9.53 | 11.13 | 15.09 | 12.70 | 19.05 | 23.83 | 27.79 | 31.75 | 35.71 | |
| 16 | 400 | 406.4 | 4.19 | 6.35 | 7.92 | 9.53 | 9.53 | 12.70 | 16.66 | 12.70 | 21.44 | 26.19 | 30.96 | 36.53 | 40.49 | |
| 18 | 450 | 457 | 4.19 | 6.35 | 7.92 | 11.13 | 9.53 | 14.27 | 19.05 | 12.70 | 23.83 | 29.36 | 34.93 | 39.67 | 45.24 | |
| 20 | 500 | 508 | 4.78 | 6.35 | 9.53 | 12.70 | 9.53 | 15.09 | 20.62 | 12.70 | 26.19 | 32.54 | 38.10 | 44.45 | 50.01 | |
| 22 | 550 | 559 | 4.78 | 6.35 | 9.53 | 12.70 | 9.53 | 22.23 | 12.70 | 28.58 | 34.93 | 41.28 | 47.63 | 53.98 | ||
| 24 | 600 | 610 | 5.54 | 6.35 | 9.53 | 14.27 | 9.53 | 17.48 | 24.61 | 12.70 | 30.96 | 38.89 | 46.02 | 52.37 | 59.54 | |
| 26 | 650 | 660 | 7.92 | 12.70 | 9.53 | 12.70 | ||||||||||
ASTM A53 Standard Steel Grades
ASTM A53 Grade A
ASTM A53 Grade A steel pipe The minimum yield strength is 205 MPa. It is suitable for fluid transportation such as oil and gas, and the mechanical strength requirements are general application scenarios.
ASTM A53 Grade B steel pipe Minimum yield strength 240 MPa. It is suitable for applications requiring higher mechanical strength.
ASTM A53 Production Tolerance
ASTM A53 carbon steel pipe standard, its manufacturing process tolerance control, to ensure the quality, safety and reliability of the steel pipe production. Tolerances usually include outer diameter tolerances, wall thickness tolerances, length tolerances, ellipticity, straightness, etc.
| Weight (mass)-of the pipe shall not vary more than 6 10 % from its specified weight (mass), as derived by multiplying its measured length by its specified weight (mass) per unit length, as given in Table X2.2 or Table X2.3, or as calculated using the relevant equation in ASME B36.10M. |
| Thickness—The minimum wall thickness at any point shall be not more than 12.5 % under the specified wall thickness. The minimum wall thickness on inspection shall conform to the requirements given in Table X2.4. |
| Diameter—For pipe NPS 11⁄2 [DN 40] or smaller, the outside diameter at any point shall not vary more than 6 1⁄64 in. [0.4 mm] from the specified outside diameter. For pipe NPS 2 [DN 50] or larger, the outside diameter shall not vary more than 6 1 % from the specified outside diameter. |
ASTM A53 Chemical Composition
Pandapipe offers to manufacture ASTM A53 steel pipes in strict accordance with standard specifications, selecting steel with the correct chemical composition as the raw material to guarantee the strength, durability and corrosion resistance of the pipes. Its chemical composition includes elements such as carbon, silicon, manganese, phosphorus and sulfur. Each element composition is carefully controlled to ensure the quality and performance of the pipe.
| A53/A53M − Chemical Requirements | |||||||||
| Composition, max, % | |||||||||
| Carbon | Manganese | Phosphorus | Sulfur | CopperA | NickelA | ChromiumA | MolybdenumA | VanadiumA | |
| Type S (seamless pipe) | |||||||||
| Grade A Grade B | 0.25B 0.30C | 0.95 1.20 | 0.05 0.05 | 0.045 0.045 | 0.40 0.40 | 0.40 0.40 | 0.40 0.40 | 0.15 0.15 | 0.08 0.08 |
| Type E (electric-resistance-welded) | |||||||||
| Grade A Grade B | 0.25B 0.30C | 0.95 1.20 | 0.05 0.05 | 0.045 0.045 | 0.40 0.40 | 0.40 0.40 | 0.40 0.40 | 0.15 0.15 | 0.08 0.08 |
| Type F (furnace-welded pipe) | |||||||||
| Grades A and B | 0.30B | 1.2 | 0.05 | 0.045 | 0.4 | 0.4 | 0.4 | 0.15 | 0.08 |
| A The total composition for these five elements shall not exceed 1.00 %. | |||||||||
| B For each reduction of 0.01 % below the specified carbon maximum, an increase of 0.06 % manganese above the specified maximum will be permitted up to a maximum of 1.35 %. | |||||||||
| C For each reduction of 0.01 % below the specified carbon maximum, an increase of 0.06 % manganese above the specified maximum will be permitted up to a maximum of 1.65 %. | |||||||||
ASTM A53 Mechanical Properties
The ASTM A53 carbon steel pipe we manufacture has passed the standard requirements of tensile strength, yield strength, elongation and other performance requirements, ensuring that each pipe is strictly certified, get toughness and stiffness, and ensure the safety and durability of the project.
| Tensile Requirements | ||
|---|---|---|
| Grade A | Grade B | |
| Tensile strength, min, psi [MPa] | 48 000 [330] | 60 000 [415] |
| Yield strength, min, psi [MPa] | 30 000 [205] | 35 000 [240] |
| Elongation in 2 in. or 50 mm | A,B | A,B |
| ||

The table lists minimum elongation values in inch-pounds.Minimum elongation values in inch-pounds.
| Area,A,in.² | Specified Wall Thickness,in. | Elongation in 2 in,min,% | |||
| Tension Test Specimen | Specified Minimum Tensile Strength,psi | ||||
| Y4-in. | 1-in. | 12-in. | |||
| Specimen | Specimen | Specimen | 48000 | 60000 | |
| 0.75 and | 0.994 and | 0.746 and | 0.497 and | 36 | 30 |
| greater | greater | greater | greater | ||
| 0.74 | 0.980-0.993 | 0.735-0.745 | 0.490-0.496 | 36 | 29 |
| 0.73 | 0.967-0.979 | 0.726-0.734 | 0.484-0.489 | 36 | 29 |
| 0.72 | 0.954-0.966 | 0.715-0.725 | 0.477-0.483 | 36 | 29 |
| 0.71 | 0.941-0.953 | 0.706-0.714 | 0.471-0.476 | 36 | 29 |
| 0.70 | 0.927-0.940 | 0.695-0.705 | 0.464-0.470 | 36 | 29 |
| 0.69 | 0.914-0.926 | 0.686-0.694 | 0.457-0.463 | 36 | 29 |
| 0.68 | 0.900-0.913 | 0.675-0.685 | 0.450-0.456 | 35 | 29 |
| 0.67 | 0.887-0.899 | 0.666-0.674 | 0.444-0.449 | 35 | 29 |
| 0.66 | 0.874-0.886 | 0.655-0.665 | 0.437-0.443 | 35 | 29 |
| 0.65 | 0.861-0.873 | 0.646-0.654 | 0.431-0.436 | 35 | 29 |
| 0.64 | 0.847-0.860 | 0.635-0.645 | 0.424-0.430 | 35 | 29 |
| 0.63 | 0.834-0.846 | 0.626-0.634 | 0.417-0.423 | 35 | 29 |
| 0.62 | 0.820-0.833 | 0.615-0.625 | 0.410-0.416 | 35 | 28 |
| 0.61 | 0.807-0.819 | 0.606-0.614 | 0.404-0.409 | 35 | 28 |
| 0.60 | 0.794-0.806 | 0.595-0.605 | 0.397-0.403 | 35 | 28 |
| 0.59 | 0.781-0.793 | 0.586-0.594 | 0.391-0.396 | 34 | 28 |
| 0.58 | 0.767-0.780 | 0.575-0.585 | 0.384-0.390 | 34 | 28 |
| 0.57 | 0.754-0.766 | 0.566-0.574 | 0.377-0.383 | 34 | 28 |
| 0.56 | 0.740-0.753 | 0.555-0.565 | 0.370-0.376 | 34 | 28 |
| 0.55 | 0.727-0.739 | 0.546-0.554 | 0.364-0.369 | 34 | 28 |
| 0.54 | 0.714-0.726 | 0.535-0.545 | 0.357-0.363 | 34 | 28 |
Application of ASTM A53
Oil and gas industry: Because ASTM A53 has excellent corrosion resistance and safety. It is often used for pipeline transportation such as oil and gas.
Chemical industry: ASTM A53 is widely used in acid and base solution transportation, chemical gas transmission and other processes. It is also commonly used for structural support and load-bearing components.
Construction industry: ASTM A53 light weight, high strength, short construction period. It is often used in construction frames, support structures and Bridges.
FAQs:
1.ASTM A53 Grade B Pipe Weight
Pipe weight calculation formula: Steel pipe weight (kg/m) = [Outer diameter (mm) – Wall thickness (mm)] × Wall thickness (mm) × 0.02466 (Converted from carbon steel density 7.85 g/cm³).
Weight of common specifications
| Nominal Pipe Size (NPS) | Outer diameter (mm) | Wall thickness (mm) | Theoretical weight (kg/m) |
|---|---|---|---|
| 1/2″ | 21.3 | 2.77 | 1.27 |
| 1″ | 33.4 | 3.38 | 2.50 |
| 2″ | 60.3 | 3.91 | 5.44 |
| 4″ | 114.3 | 6.02 | 16.07 |
| 6″ | 168.3 | 7.11 | 28.41 |
2.What is the difference between AMS and ASTM?
ASTM, issued by the American Society for Testing and Materials, covers a broad range of standards and is applicable to general industry.
AMS, issued by the Society of Automotive Engineers International, is specifically used in aerospace applications.
3.ASTM A53 Hydrostatic Testing Process
First, fill the pipe with water and ensure it is vacuum-free. Install a pressure gauge and connect a pressure pump. Apply pressure to the pipe to its maximum value for at least five seconds. If the pipe shows no deformation or leakage after the pressure is applied, it has passed the water pressure test.
 English
 Deutsch
 Español
 Português
 Nederlands
 Italiano
 Français
 Русский
 Українська
 العربية
 日本語
 한국어
 Bahasa Indonesia